CNMG vs TNMG vs WNMG Inserts: Differences Explained
Nov. 17, 2026
CNMG is generally the strongest choice for heavy roughing, TNMG suits lighter finishing and profiling, and WNMG combines an 80-degree corner with six usable cutting edges. The practical difference comes from shape, included angle, clearance, edge strength, accessibility, chip control, and how the holder presents the insert to the workpiece.
!
When I compare CNMG vs TNMG vs WNMG inserts, I do not treat the insert shape as an isolated specification. The correct selection also depends on material, depth of cut, feed rate, machine size, toolholder rigidity, nose radius, chipbreaker design, coating, and the required surface finish. This guide explains the geometric differences and provides a practical selection method for CNC machinists, job shops, and production users.
Key Takeaways
- CNMG inserts provide the highest edge strength for heavy roughing, interrupted cuts, and large depths of cut.
- TNMG inserts offer six nominal cutting edges and better access for profiling, shoulders, and restricted turning areas.
- WNMG inserts combine an 80-degree corner with six usable edges for general turning and moderate roughing.
- Actual usable edges depend on holder orientation, clearance, chipbreaker design, and whether both insert sides remain accessible.
- Insert shape must be selected separately from carbide grade, coating, nose radius, and chipbreaker geometry.
What Are CNMG, TNMG, and WNMG Inserts?
CNMG, TNMG, and WNMG are ISO-style carbide turning insert designations. The first letter identifies the insert shape, while the second letter identifies the clearance angle beneath the cutting edge. In all three cases, the “N” indicates 0-degree clearance, so these are negative-rake insert families intended for compatible negative-style holders.
The first letter creates the main difference. “C” identifies an 80-degree diamond, “T” identifies a 60-degree triangle, and “W” identifies an 80-degree trigon. The remaining code characters describe tolerance class, hole and chipbreaker configuration, insert size, thickness, and nose radius.
| Insert | Basic shape | Included corner angle | Clearance | Nominal usable edges | Typical role |
|---|---|---|---|---|---|
| CNMG | 80-degree diamond | 80° | 0° | 4 | Heavy roughing and general external turning |
| TNMG | Triangle | 60° | 0° | 6 | Profiling, finishing, shoulders, and general turning |
| WNMG | Trigon | 80° | 0° | 6 | General turning, moderate roughing, and repeated indexing |
The listed edge counts describe the standard insert design, not an unconditional guarantee that every corner will be practical in every setup. A holder may block a corner, reduce clearance near a shoulder, or prevent the opposite face from being indexed without removing the insert. I therefore distinguish between the theoretical edge count and the number of edges that can be used effectively in a particular holder.
CNMG vs TNMG vs WNMG Inserts: Key Differences
Geometry and cutting-edge strength
CNMG has an 80-degree diamond shape with a comparatively wide included corner. That geometry supports a strong cutting point and distributes cutting forces through a substantial body of carbide. I normally consider CNMG when the operation involves a large depth of cut, higher feed, scale, forging skin, or interrupted engagement.
TNMG uses a 60-degree triangular shape. The sharper point reaches internal corners and shoulders more easily than the 80-degree corners of CNMG and WNMG, but the smaller included angle leaves less carbide behind the cutting edge. TNMG can therefore provide better access and lower cutting resistance, although it is generally less tolerant of severe impact or excessive feed.
WNMG uses an 80-degree trigon shape. Its corner strength is closer to CNMG than TNMG because the working corner has an 80-degree included angle, while the three-corner layout on both sides provides six nominal cutting edges. This makes WNMG a useful compromise for shops that want repeated indexing without moving immediately to the heavier CNMG format.
Edge count and holder access
A standard CNMG insert normally provides four usable cutting edges because each side contributes two indexable corners. TNMG and WNMG designs normally provide six nominal cutting edges because each side contributes three corners. That difference affects cost per edge, but it should not be used as the only purchasing criterion.
The holder determines whether those edges can be used without interference. For example, a CNMG holder may expose the selected corner clearly during external turning, while another setup may place the insert close to a shoulder where the side clearance becomes restrictive. TNMG often offers better point access, but its 60-degree tip may be more vulnerable when the holder, workpiece, or toolpath creates impact.
Rigidity and cutting forces
Negative inserts require a holder and machine setup capable of handling their cutting forces. The 0-degree clearance geometry creates a strong seating arrangement, but the cutting edge is not as free-cutting as a positive-rake insert. On a rigid CNC lathe with a short tool overhang, this can support stable roughing at a suitable feed and depth of cut.
A small machine with limited spindle power may respond differently. If the insert is too large, the depth of cut is too aggressive, or the chipbreaker is intended for a heavier range, the result may be spindle overload, vibration, or poor chip formation. In those conditions, a smaller TNMG or a positive-rake insert can reduce cutting resistance more effectively than simply changing carbide grade.
Typical applications
CNMG is commonly selected for external roughing, facing, scale removal, cast surfaces, and general turning where edge strength takes priority. It also works well for production operations that repeat the same roughing pass and require predictable indexing. A suitable chipbreaker and grade are still necessary because the shape alone does not control crater wear, built-up edge, or thermal cracking.
TNMG is often used for profiling, light shoulder work, finishing passes, and applications where the tool must reach a contour with limited interference. Its 60-degree point can provide access to features that an 80-degree insert cannot reach without changing the toolpath. TNMG is not automatically a finishing insert; surface finish depends on feed, nose radius, toolpath, edge preparation, and chipbreaker selection.
WNMG is suited to general-purpose external turning, moderate roughing, facing, and repeat production where six indexing positions are valuable. It provides more corner positions than CNMG while retaining an 80-degree corner angle. I often regard it as a practical middle option when the operation is too demanding for a sharp TNMG point but does not require the full roughing orientation of CNMG.
Application Guide: Roughing, Finishing, Facing, and Boring
For heavy roughing, I usually start with CNMG when the machine, holder, and workholding can support the required cutting load. A typical roughing setup may use a nose radius from 0.8 to 1.6 mm, a roughing chipbreaker, and a carbide grade matched to the workpiece material. The final cutting speed and feed must come from the insert manufacturer’s data and then be reduced or increased after checking spindle load, vibration, and chip shape.
For finishing, TNMG may be preferable when the profile contains shoulders, tapers, or restricted access. However, a WNMG or CNMG with a smaller nose radius can also produce an acceptable finish if the holder orientation and feed are correct. For a theoretical turning finish, feed and nose radius are related approximately by Ra ≈ f²/(32r), where f is feed per revolution and r is nose radius, but real results also depend on material, edge condition, vibration, and insert geometry.
For facing, CNMG provides a strong corner for stock removal near the center-to-outer-diameter transition, especially on rigid machines. WNMG can handle many routine facing operations and offers six nominal edges. TNMG is useful when the face contains a narrow step or a contour requiring a sharper point, but the toolpath should avoid sudden impact at the outer edge.
For boring, accessibility becomes more important than the insert’s nominal edge strength. TNMG can reach smaller internal features and profile transitions more easily, but the boring bar must remain sufficiently rigid. CNMG and WNMG may be selected for larger internal diameters where the bar diameter, overhang, and available clearance support the insert body.
Material compatibility
For carbon steel and alloy steel, CNMG and WNMG are common starting points for roughing because their 80-degree corners tolerate higher mechanical loading. TNMG can be used for steel finishing or profiling when the depth of cut and feed remain within the selected chipbreaker range. A coated carbide grade designed for steel is usually more important than choosing one shape universally.
For stainless steel, chip control and edge-line stability become critical because work hardening can occur if the insert rubs instead of cutting. A positive-rake geometry may be preferable on smaller machines or thin sections, while a negative TNMG, WNMG, or CNMG can work on a rigid setup with an appropriate stainless-steel chipbreaker.
For cast iron, CNMG is often suitable for interrupted or abrasive surfaces when the insert grade and edge preparation support impact resistance. WNMG can provide a useful balance for general turning, while TNMG should be protected from direct shock at the 60-degree point. For aluminum, a sharp positive-rake insert is usually more appropriate than a conventional negative CNMG, TNMG, or WNMG because aluminum benefits from lower cutting resistance and a polished cutting edge.
How to Read Carbide Insert Codes
A code such as CNMG 120408 contains several pieces of information. “C” identifies the 80-degree diamond shape, “N” indicates 0-degree clearance, “M” identifies the tolerance class, and “G” identifies the hole and chipbreaker configuration. The remaining digits identify the insert size, thickness, and nose radius.
The final two digits are commonly interpreted as the nose-radius code. In 120408, “08” normally represents a 0.8 mm nose radius, while “04” commonly represents the thickness code. The first two digits describe the inscribed-circle size in the manufacturer’s coding system, but the exact dimensional interpretation should be checked against the supplier’s catalog because code tables can vary by insert standard and product family.
The same method applies to TNMG and WNMG codes. For example, TNMG 160408 and WNMG 080408 identify different shapes and sizes even though both end in “08,” meaning the nose-radius portion is commonly 0.8 mm. Code identification is only the starting point; I also verify the holder, chipbreaker range, grade, coating, and cutting-data table before placing an insert into production.
Failure Modes, Chipbreakers, and Carbide Grades
Insert failure often reveals a mismatch between geometry and operating conditions. A chipped corner may result from interrupted cutting, excessive feed, poor workholding, or a grade with insufficient impact resistance. Flank wear usually points toward abrasive material, excessive cutting speed, or inadequate coolant control, while built-up edge can indicate low cutting speed, a dull edge, poor chipbreaker selection, or material-specific adhesion.
The chipbreaker must match the depth of cut and feed range. A finishing chipbreaker is not designed to absorb the same load as a roughing chipbreaker, even when both are available on the same CNMG, TNMG, or WNMG shape. I select the chipbreaker after identifying the material and cutting range, then confirm that the expected chip thickness falls inside the supplier’s recommended window.
Carbide grade and coating should be selected separately from insert shape. A steel grade, stainless-steel grade, cast-iron grade, or non-ferrous grade may use the same external shape but differ in substrate, coating layers, edge preparation, and recommended speed range. Changing from TNMG to CNMG will not correct a coating problem, and changing from an uncoated grade to a coated grade will not solve an inaccessible toolpath.
A positive-rake insert is preferable when spindle power is limited, the workpiece is thin, the boring bar is small, or the machine cannot maintain rigidity under negative-rake cutting. Positive inserts generally reduce cutting resistance and can improve chip evacuation in aluminum and some stainless-steel applications. The tradeoff is reduced edge support, so they require better control of impact, workholding, and tool overhang.
Practical Decision Matrix
| Operating condition | Preferred starting shape | Reason |
|---|---|---|
| Heavy external roughing | CNMG | Strong 80° corner and stable support |
| Moderate roughing with six edges | WNMG | Six nominal edges with an 80° corner |
| Profile turning and restricted access | TNMG | 60° point reaches contours more easily |
| Large interrupted cut | CNMG | Greater corner support than TNMG |
| Small CNC lathe with limited power | TNMG or positive-rake insert | Lower cutting resistance and better access |
| General steel turning | WNMG or CNMG | Balanced edge strength and indexing economy |
| Fine profile finishing | TNMG | Point access and smaller available nose-radius options |
| Large internal boring | CNMG or WNMG | Depends on bar diameter and internal clearance |
| Aluminum turning | Positive-rake insert | Lower resistance and reduced built-up-edge risk |
| Cast-iron roughing | CNMG | Better tolerance of abrasive and interrupted surfaces |
Worked Example: Choosing an Insert for One Part
Suppose I am machining a 100 mm diameter alloy-steel shaft on a rigid CNC lathe. The operation removes 3 mm radially in a roughing pass, uses a feed of 0.25 mm/rev, and leaves a 0.3 mm finishing allowance. The part includes one shallow shoulder and a short external radius, but no deep internal bore.
For the roughing pass, I would begin with CNMG because the 80-degree corner provides better support at a 3 mm radial depth of cut and a 0.25 mm/rev feed. I would pair it with a steel roughing chipbreaker, a grade intended for alloy steel, and a nose radius around 0.8 or 1.2 mm, subject to the manufacturer’s data and machine power.
For the finishing pass around the shoulder and radius, I might change to TNMG if the toolpath requires closer access to the profile. If the shoulder is open and the production plan favors fewer insert changes, WNMG could finish the part instead. The decision is not based on shape alone; I would check the required surface-finish value, the actual feed, the nose radius, holder clearance, and whether the remaining stock is consistent.
This example shows why CNMG vs TNMG vs WNMG inserts are not competing choices with one universal winner. The same part can require CNMG for roughing and TNMG for profiling, while WNMG may reduce tool changes when the geometry and finish requirements are moderate.
CNMG vs TNMG Insert Differences and Holder Compatibility
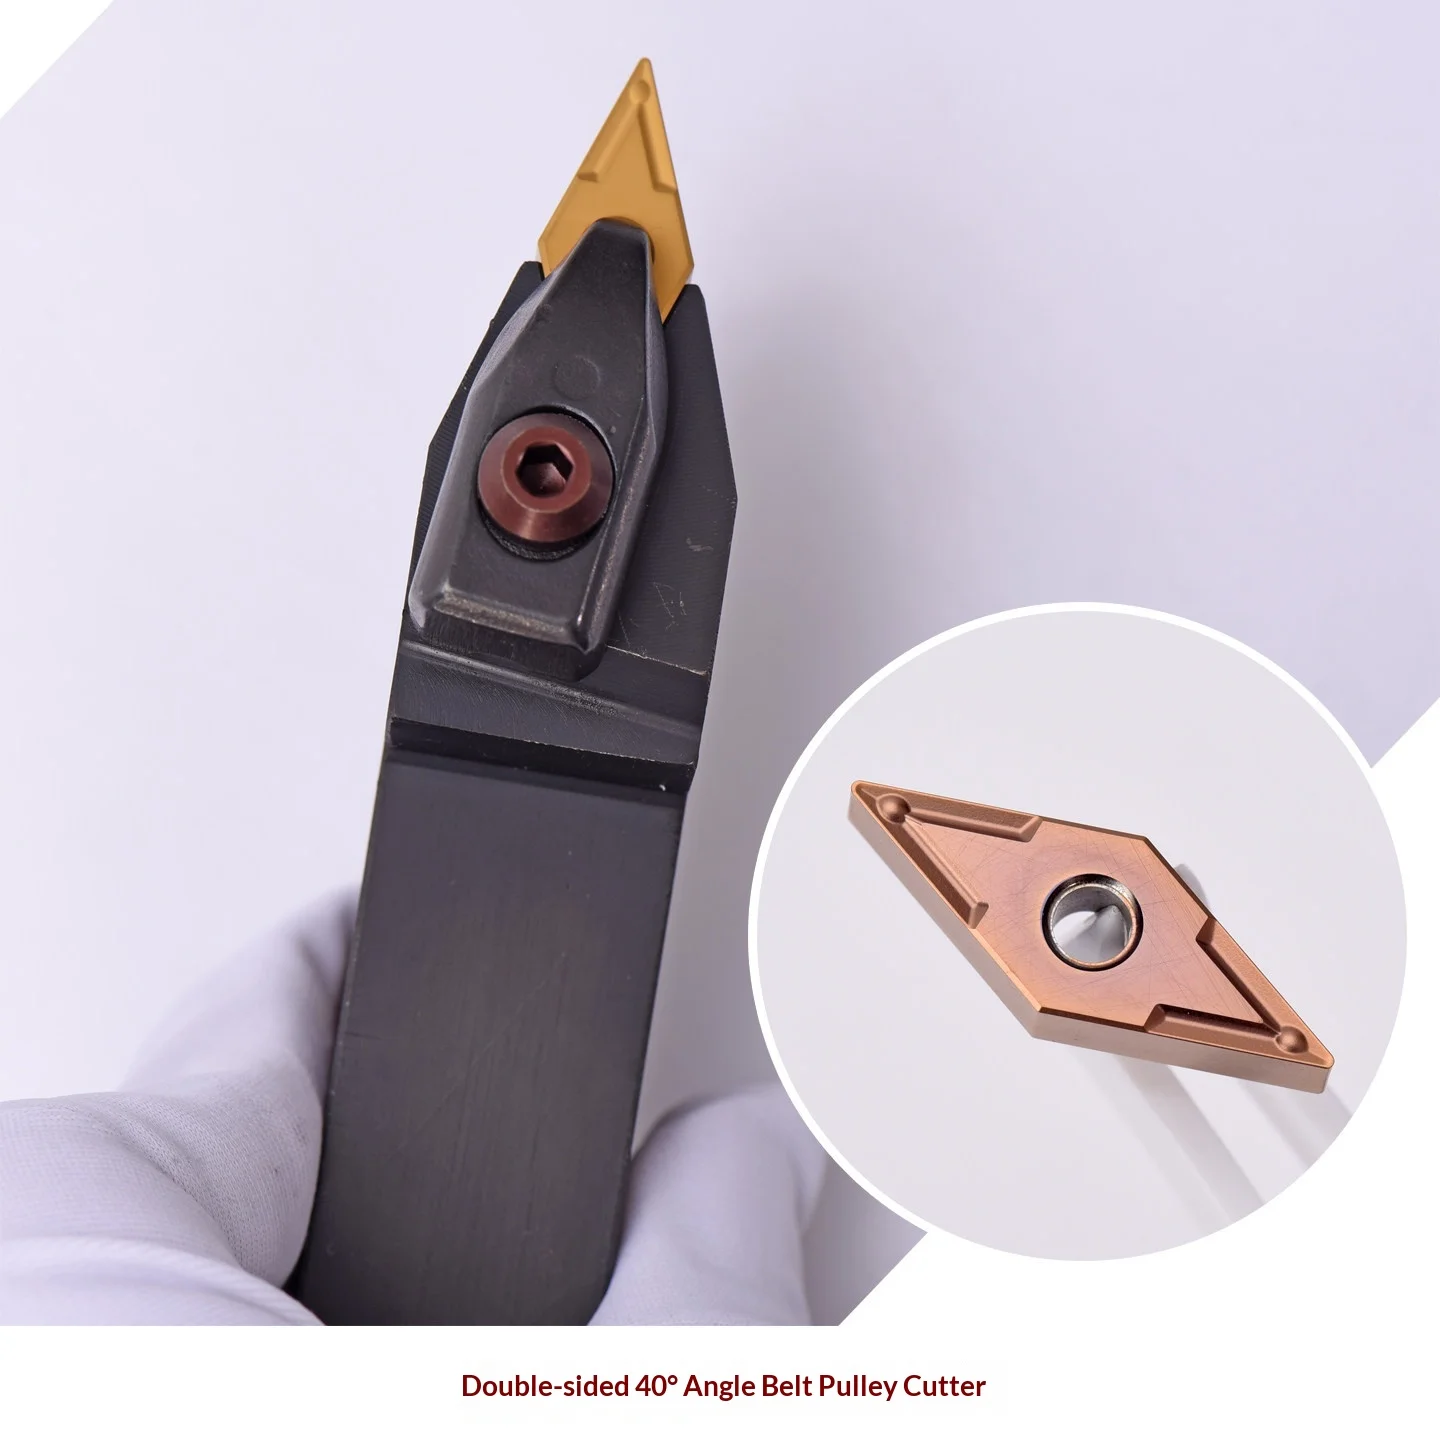
CNMG, TNMG, and WNMG inserts do not automatically use the same toolholder. The holder must match the insert shape, seating geometry, screw or clamp arrangement, hand orientation, and cutting approach angle. Even when two inserts share a nominal size, their support surfaces and exposed cutting corners can differ.
I check the complete holder designation before ordering replacement inserts. The holder must provide adequate seating beneath the insert, maintain the intended lead angle, and leave sufficient clearance for the workpiece, chuck, shoulder, and chip flow. Installing an insert into an incompatible holder can produce incorrect cutting geometry, unstable seating, or interference with the workpiece.
KEUE CNC supplies Turning Inserts, CNC toolholders, boring tools, milling products, drilling tools, and related tooling systems. The company describes its operation as established in 2011, with a manufacturing site in Wenling, Taizhou, China, an approximately 10-acre factory area, an independent R&D and design team, and exports reaching more than 100 countries. Its stated customization process includes reviewing product or workpiece drawings, confirming coating, size, and precision requirements, and providing quoted delivery timing that can be as short as 3–7 days for customized products.
For a buyer comparing insert families, this type of supplier information matters because the product decision often includes more than loose carbide inserts. Holder compatibility, custom dimensions, coatings, technical support, and production-improvement assistance can affect the total cost of changing an insert system. I would still request the exact grade chart, dimensional drawing, chipbreaker range, and sample cutting data before approving a new insert for production.
How to Choose the Right CNC Turning Insert
I use the following sequence when selecting among CNMG, TNMG, and WNMG:
- Identify the operation. Separate roughing, finishing, facing, profiling, and boring rather than choosing one shape for every pass.
- Measure the cutting range. Record depth of cut, feed per revolution, workpiece diameter, stock variation, and interrupted-cut conditions.
- Check machine and setup rigidity. Include spindle power, workholding, tool overhang, boring-bar diameter, and turret stability.
- Select the shape. Start with CNMG for heavy roughing, TNMG for access and profiling, or WNMG for general turning with six nominal edges.
- Select nose radius and chipbreaker. Match the nose radius to feed, finish, and corner access, then match the chipbreaker to chip thickness.
- Select grade and coating. Use material-specific recommendations for steel, stainless steel, cast iron, aluminum, or high-temperature alloys.
- Confirm the holder. Verify insert size, clamp system, approach angle, hand, clearance, and actual indexable corners.
- Run a controlled test. Record tool life, spindle load, chip shape, surface roughness, edge wear, and parts completed per edge.
Final Thoughts
CNMG vs TNMG vs WNMG Inserts: Differences Explained comes down to a balance between edge strength, access, edge count, cutting load, and application requirements. CNMG is generally the safest starting point for heavy roughing, large depths of cut, and interrupted external turning. TNMG is usually more practical for finishing, profiling, shoulders, and restricted-access areas, while WNMG provides an 80-degree corner with six nominal usable edges for general turning and moderate roughing.
I recommend selecting the geometry first, then choosing the nose radius, chipbreaker, carbide grade, coating, and holder. For small CNC lathes, thin workpieces, aluminum, or weak boring setups, a positive-rake insert may be preferable to any conventional negative CNMG, TNMG, or WNMG design. For production machining, compare actual usable edges rather than theoretical counts, and validate the choice through spindle load, chip control, surface finish, and tool-life records.