CNC Cutting Tool Trends in 2026: What Buyers Should Watch
Nov. 16, 2026
CNC Cutting Tool Trends in 2026: What Buyers Should Watch center on smart tooling, advanced coatings, adaptive monitoring, difficult-material machining, and lower-impact production. Buyers are moving beyond tool price and comparing measurable results such as tool life, cycle time, scrap rate, cost per component, data compatibility, and payback period.
!
CNC Cutting Tool Trends in 2026 Buyers Need to Understand
I see the 2026 market shifting from isolated tool purchases toward connected machining systems. A cutting tool is no longer evaluated only by insert price or catalog geometry; it is increasingly judged by how well it works with the machine controller, toolholder, CAM software, coolant system, inspection equipment, and production database. This change affects small machine shops as well as aerospace, automotive, energy, and medical manufacturers.
The most important buying criteria are:
- Application fit: Match the substrate, coating, edge preparation, flute geometry, and toolholder to the workpiece material and cutting operation.
- Measured productivity: Compare tool life, cutting speed, feed rate, cycle time, scrap rate, and cost per component rather than relying on unit price.
- Digital compatibility: Check whether tool data, presetting information, wear records, and machine signals can move between planning and production systems.
- Technical support: Confirm whether the supplier provides cutting-data recommendations, application testing, regrinding, troubleshooting, and replacement planning.
- Total cost of ownership: Include tool changes, setup time, rejected parts, downtime, inventory, coolant consumption, and operator intervention.
What Are the Biggest CNC Cutting Tool Trends in 2026?
The biggest trends are smart CNC cutting tools, advanced carbide and ceramic grades, application-specific coatings, adaptive control, automated tool handling, five-axis machining, difficult-material capability, and sustainability. These trends are connected because manufacturers want higher material-removal rates without sacrificing dimensional control or increasing tool-related downtime.
A useful way to understand the market is to separate the trends into five operating priorities: collecting process data, increasing unattended production, machining harder materials, improving tool life, and reducing waste. Each priority requires a different product decision. For example, a sensor-enabled holder may help detect overload, while a PCD tool may be the correct choice for high-volume aluminum machining.
1. Smart CNC Cutting Tools Are Moving From Monitoring to Decision Support
Smart CNC cutting tools use sensors, machine signals, presetting data, or software algorithms to identify wear, overload, vibration, and tool breakage. In practical terms, the system may monitor spindle load, acoustic emissions, vibration, cutting time, feed override, or power consumption. The purpose is not to collect data for its own sake; the purpose is to make a timely production decision.
A basic tool-monitoring program can trigger an alarm when a tool exceeds a defined load or cutting-time threshold. A more advanced system can estimate remaining tool life and recommend a replacement before the tool causes burrs, dimensional drift, or breakage. Siemens, for example, describes adaptive control systems that adjust feed rates in real time and monitor tool overload, wear, and breakage.
For buyers, the important question is whether the system connects to existing equipment. Ask whether it supports the machine controller, OPC UA or another plant data interface, tool presetting software, and the shop’s manufacturing execution system. A system that requires manual transcription of tool data may create additional work instead of reducing it.
The financial case should be calculated using production data. If a monitoring system costs $8,000 and reduces one $1,200 scrap event per month while saving 10 minutes per cycle across 400 cycles, the payback period may be under one year depending on the machine-hour rate. Buyers should calculate payback from actual avoided losses rather than from predicted tool-life percentages alone.
2. Advanced CNC Tool Coatings Improve Heat and Wear Control
Advanced CNC tool coatings are becoming more application-specific. Common coating families include TiN, TiCN, TiAlN, AlTiN, diamond coatings, and multilayer PVD or CVD structures. Their functions differ: some reduce friction, some resist abrasive wear, some protect the substrate at elevated temperatures, and others are designed for non-ferrous materials.
How Do Advanced CNC Tool Coatings Improve Performance?
Coatings improve performance by creating a harder, chemically stable surface between the cutting edge and the workpiece. In high-speed machining, the coating can delay flank wear, crater wear, built-up edge, and thermal damage, but the result depends on cutting speed, feed, coolant, workpiece chemistry, and edge geometry.
A coating is not automatically suitable for every material. Aluminum often requires a sharp, low-friction edge and may benefit from a polished flute or diamond coating, while hardened steel commonly requires a wear-resistant carbide grade with a coating designed for heat. Titanium and nickel-based alloys require careful control of heat generation, chip evacuation, and radial engagement.
Buyers should request test data using the intended material and operation. A meaningful comparison records tool life in minutes or parts, dimensional drift, surface roughness, cutting parameters, and failure mode. If one coated end mill lasts 42 minutes at 180 meters per minute while another lasts 31 minutes at the same feed and engagement, the comparison is more useful than a general claim about coating hardness.
3. Carbide Grades and Edge Geometries Are Becoming More Specialized
Carbide remains the default material for many CNC cutting tools because it offers a practical balance of hardness, toughness, wear resistance, and cost. However, carbide grades are increasingly selected by application instead of being treated as interchangeable products. A roughing operation in cast iron, a finishing pass in hardened steel, and a high-speed aluminum cut require different substrate and edge characteristics.
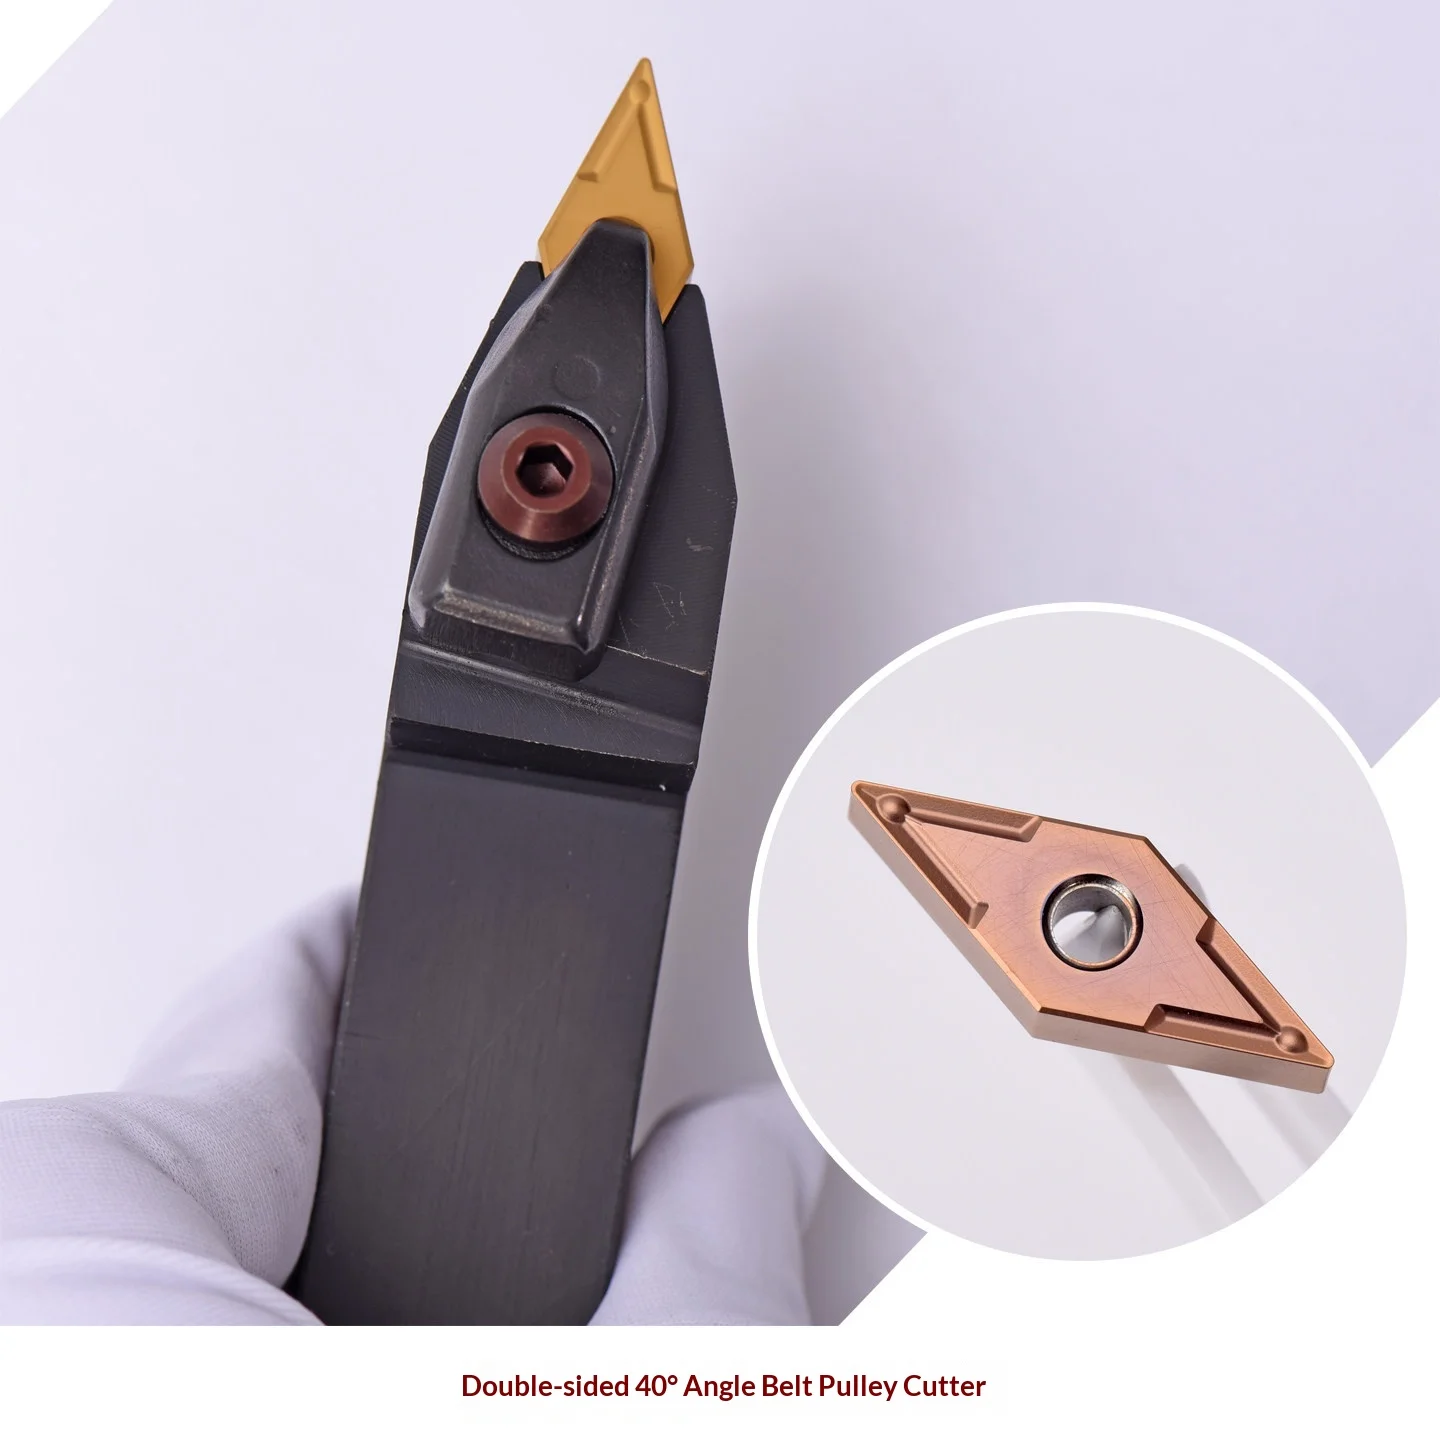
For difficult materials, buyers may need ceramic, CBN, or PCD tools. Ceramic tools can support high cutting speeds in selected hardened steels and nickel alloys, but they generally require stable setups and controlled engagement. CBN is used for hardened ferrous materials, while PCD is widely considered for abrasive non-ferrous alloys, graphite, wood-based composites, and high-volume aluminum applications.
Edge geometry also has a direct effect on process stability:
- Sharp edges reduce cutting force and are useful for aluminum, copper, and thin-wall components.
- Honed edges resist chipping during general steel machining and moderate interruptions.
- Chamfered edges provide additional edge strength for heavy cuts and unstable conditions.
- Variable-pitch flutes help reduce harmonic vibration in milling.
- High-feed geometries use a small entering angle to increase feed per tooth while controlling cutting forces.
I recommend asking the supplier to explain the intended failure mode. If the current tool fails through edge chipping, a tougher grade or stronger edge preparation may be required. If it fails through gradual flank wear, a more wear-resistant substrate or coating may deliver a better result.
4. Automation and Robotics Are Changing Tool Handling
Automation is expanding beyond part loading and unloading. In 2026, manufacturers are also automating tool presetting, tool identification, insert replacement, tool vending, regrinding schedules, and tool-life records. These systems reduce the number of manual decisions required between machining operations.
Robotic tool handling is most useful where production involves repeated tool changes, multiple machines, or long unattended shifts. A robot can transfer preset tools to a machine, return worn tools for inspection, and maintain a digital record of tool identity. The value depends on production volume and labor cost; a low-volume job shop may gain more from standardized presetting than from a full robotic cell.
The productivity calculation should include tool-change time. For example, reducing 90 seconds from each of 30 tool changes per shift saves 45 minutes per shift. At a machine cost of $75 per hour, that represents $56.25 of potential capacity per shift before considering labor, maintenance, and integration costs.
Automation also places greater demands on consistency. Toolholders must maintain repeatable runout, preset dimensions must be accurate, insert screws and clamping components must be controlled, and replacement tools must match the programmed specification. A variation of 0.01 mm in tool length or radial runout can matter in finishing operations with tight tolerance requirements.
5. Five-Axis Machining and Adaptive Control Are Expanding Precision Capability
Five-axis machining is not becoming universal, but it is becoming more common for parts with complex surfaces, deep features, short setup windows, or difficult access angles. Aerospace blisks, turbine components, medical implants, molds, and impellers often benefit from simultaneous or indexed multi-axis machining.
The main benefits are fewer setups, improved tool access, shorter tool overhang, and better control of the cutter contact point. These improvements can reduce cumulative setup error, but they require qualified postprocessors, collision checking, machine calibration, and toolholders designed for the required spindle speed.
Adaptive control adds another layer. The control system can adjust feed rate based on spindle load, cutting force, vibration, or material engagement. During air cutting, it may increase feed; during heavy engagement, it may reduce feed to avoid overload. This approach can shorten cycle time while protecting the tool from sudden cutting-condition changes.
Buyers should not assume that adaptive control will compensate for poor tool selection. The tool geometry, workholding, coolant delivery, and toolpath still determine the basic process. Adaptive systems are most useful when the process is already stable but contains variable stock, interrupted cuts, or changing engagement.
6. Difficult Materials Are Driving New Tool Development
Aerospace and energy manufacturers are increasing their use of titanium alloys, nickel-based superalloys, hardened steels, carbon-fiber composites, silicon-rich aluminum, and other abrasive or heat-sensitive materials. These materials place different demands on cutting tools, including resistance to heat, adhesion, edge chipping, abrasive wear, and poor chip evacuation.
For titanium, buyers should evaluate sharp but supported edges, controlled cutting speeds, high-pressure coolant where appropriate, and toolpaths that limit heat concentration. Nickel-based alloys often require strong thermal management and conservative engagement because the material can retain heat near the cutting zone.
Carbon-fiber composites create abrasive wear and may delaminate if the tool geometry is unsuitable. PCD or diamond-coated tools may be appropriate for certain composite operations, but the buyer must also review dust extraction, edge geometry, feed direction, and part support.
The correct tool should be selected from a complete application record containing material grade, hardness, machine power, spindle speed, workholding method, coolant, tool diameter, radial engagement, axial depth, and surface-finish requirement. Without those details, a supplier comparison is incomplete.
7. Sustainability Is Becoming a Purchasing Requirement
Sustainable CNC cutting tools are being evaluated through coolant use, tool recycling, regrinding, packaging, energy consumption, and scrap reduction. Dry machining and minimum quantity lubrication can reduce fluid consumption in suitable operations, but they may increase thermal stress if the tool coating, substrate, and cutting parameters are not matched correctly.
Regrinding can extend the useful life of selected solid carbide tools. Buyers should establish an acceptable regrind limit and verify whether the reconditioned tool maintains diameter, flute geometry, coating condition, and balance. The environmental benefit should be compared with the cost of transportation, inspection, recoating, and quality control.
Sustainability also has a direct financial dimension. If a regrind costs $18 and provides 70% of the original tool life, it may reduce tooling cost for suitable roughing or semi-finishing work. If the regrind introduces dimensional variation that increases scrap by 2%, the apparent saving may disappear.
CNC Cutting Tool Life Optimization: A Buyer’s Measurement Framework
CNC cutting tool life optimization begins with a controlled baseline. I recommend recording tool life in parts and minutes, cutting speed, feed per tooth, axial and radial engagement, coolant method, tool-change time, scrap events, and the reason for tool replacement. The objective is to distinguish normal wear from damage caused by vibration, poor clamping, incorrect parameters, or chip recutting.
The most useful financial metric is cost per component:
Cost per component = tool cost + tool-change cost + scrap cost + downtime cost
For example, a $45 end mill producing 180 acceptable parts has a direct tool cost of $0.25 per part. If a parameter change increases output to 230 parts but raises scrap from 1% to 3%, the lower tool cost may not represent a lower total cost. Buyers should always evaluate the complete production result.
A practical trial should compare two or three tools under the same conditions for at least 20 to 50 parts, or until a defined wear limit is reached. Record dimensional results at regular intervals, such as every 10 parts, and establish a replacement threshold before the trial begins. This prevents the operator from extending tool use until an unexpected failure damages the workpiece or machine.
How to Evaluate CNC Cutting Tool Suppliers
I compare suppliers using four categories: product range, application support, manufacturing control, and supply continuity. A supplier should be able to provide grade recommendations, cutting data, product drawings, inspection information, replacement availability, and a clear explanation of how the tool is intended to fail.
Supplier and Product Landscape
| Supplier or resource | Main strengths | Suitable applications | Buyer questions |
|---|---|---|---|
| Sandvik Coromant | Broad indexable tooling, grades, and digital machining support | Automotive, aerospace, general production | Can the supplier provide validated data for the specific material and machine? |
| Kennametal | Carbide, ceramic, CBN, PCD, and application engineering | Difficult materials and industrial production | Are tool-life trials available for the target operation? |
| Seco Tools | Milling, turning, holemaking, and process support | General machining and production optimization | How are grades selected for interrupted or unstable cuts? |
| Mitsubishi Materials | Solid carbide, indexable tools, and material-specific grades | Precision milling, drilling, and turning | What runout, coating, and geometry options are available? |
| ISCAR | High-productivity indexable systems and modular solutions | High-feed milling, grooving, and production work | Can the system reduce tool changes or improve chip control? |
| KEUE CNC | Turning, grooving, milling, drilling, boring, holders, and customized tool options | Distributors, machine shops, aerospace, automotive, energy, and new-energy parts | What coating, size, precision, delivery time, and technical support are available? |
KEUE CNC states that it was established in 2011 in Wenling, Taizhou, China, and operates a factory covering approximately 10,000 square meters. Its listed product categories include carbide inserts, milling cutters, turning tools, grooving inserts, drills, reamers, boring tools, toolholders, collets, and face milling cutters.
For customized products, KEUE CNC describes a process based on workpiece or product drawings, tool drawing confirmation, quotation, and delivery-time discussion. The company indicates that coating, size, and precision can be customized, with quoted delivery times commonly discussed within a 3–7 day range for certain orders. Buyers should confirm the exact specification, inspection method, production quantity, and shipping schedule for each project.
What Should Buyers Look for When Purchasing CNC Equipment and Tools?
Buyers should look for compatibility between the machine, toolholder, cutting tool, monitoring system, and production objective. A tool rated for high speed is not automatically suitable if the spindle lacks sufficient power, the holder has excessive runout, or coolant cannot reach the cutting edge.
I recommend using this purchasing checklist:
- Define the material, hardness, and heat-treatment condition.
- Record spindle speed, power, torque, and maximum feed rate.
- Select tool diameter, flute count, insert geometry, and edge preparation.
- Confirm holder type, gauge length, balance rating, and runout tolerance.
- Request cutting data for speed, feed, depth of cut, and coolant.
- Establish tool-life and dimensional acceptance limits.
- Calculate cost per component and expected payback period.
- Confirm stock availability, replacement lead time, regrinding, and technical support.
- Test the tool under production conditions before approving a large order.
Conclusion
CNC Cutting Tool Trends in 2026: What Buyers Should Watch point toward connected tooling, application-specific coatings, specialized carbide grades, adaptive control, automated handling, five-axis production, and measurable sustainability. I would not select a tool based only on purchase price or a catalog statement about extended life. Instead, I would compare tool life, cycle time, scrap rate, dimensional stability, changeover time, and total cost per component under the actual machining conditions.
For a first evaluation, document the current tool’s performance across at least one production run, then test a competing grade or geometry using the same workpiece and machine settings. Include established manufacturers such as Sandvik Coromant, Kennametal, Seco Tools, Mitsubishi Materials, and ISCAR in the comparison, while also reviewing KEUE CNC for turning, milling, drilling, boring, tooling systems, customized products, and application support. The most suitable 2026 tooling strategy is the one that produces a verified payback period without increasing scrap, operator intervention, or process risk.