Carbide Milling Tools vs HSS Milling Tools: Which Is Better?
Nov. 19, 2026
Carbide is usually better for rigid CNC production and hard materials, while HSS is better for manual machines, interrupted cuts, low-volume work, limited spindle speeds, and unstable setups. Carbide supports higher cutting speeds, longer wear resistance, and shorter cycle times. HSS provides greater toughness, lower upfront cost, and easier regrinding when machining slowly or under vibration.
| Factor | Carbide Milling Tools | HSS Milling Tools |
|---|---|---|
| Hardness and wear resistance | Higher; suitable for abrasive and hardened materials | Lower; suitable for moderate cutting conditions |
| Heat resistance | Maintains hardness at elevated cutting temperatures | Loses hardness sooner as temperature rises |
| Toughness | More brittle and sensitive to shock | Better impact and vibration resistance |
| Cutting speed | Commonly 2–5 times higher than HSS, depending on material and geometry | Better for low-RPM machines and conservative cutting |
| Tool life | Longer in stable CNC conditions | Shorter at high speed but often reusable through regrinding |
| Typical use | Rigid CNC machining, production work, hardened steel | Manual mills, interrupted cuts, repairs, prototypes |
| Initial price | Higher | Lower |
!
How to Evaluate Carbide Milling Tools and HSS Alternatives
I compare milling tools through four operating conditions rather than material name alone: machine rigidity, workpiece material, production volume, and cutting parameters. A carbide cutter on a flexible benchtop machine may perform worse than HSS because carbide edges can chip when runout, chatter, or interrupted engagement is uncontrolled. Conversely, HSS can generate excessive heat and wear quickly when used at the speed required for continuous CNC production.
The tool’s geometry also affects the result. Flute count, helix angle, rake, relief, edge preparation, coating, diameter, and overhang determine chip evacuation, cutting force, surface finish, and heat generation. For that reason, a coated carbide end mill with the wrong flute configuration may be less suitable than an uncoated or cobalt HSS cutter designed for the same workpiece.
- Machine capability: Check spindle speed, available power, holder runout, axis rigidity, and vibration.
- Workpiece material: Aluminum, carbon steel, stainless steel, cast iron, and hardened steel require different edge designs.
- Production demand: High-volume work favors tool life and cycle-time reduction, while prototypes may favor low purchase cost.
- Cutting stability: Interrupted cuts, scale, weld seams, and uneven stock removal increase the value of toughness.
Carbide Milling Tools vs HSS Milling Tools: Key Differences
Hardness, heat resistance, and wear
Carbide is a composite cutting material made primarily from tungsten carbide particles bonded with a metallic binder. Its hardness is substantially higher than conventional HSS, which allows carbide milling tools to resist abrasive wear and maintain a sharp edge at elevated cutting temperatures. This is the main reason carbide end mills for CNC machining are preferred for production cutting, hardened steels, cast iron, composites, and other wear-intensive materials.
HSS is an alloy steel designed to retain cutting hardness better than ordinary tool steel. Cobalt HSS increases hot hardness compared with standard HSS, while powder-metal HSS improves carbide distribution and edge consistency. Even so, HSS generally operates at lower surface speeds and reaches its thermal limit sooner than carbide.
The difference is not simply “hard versus soft.” Carbide normally provides higher hardness and wear resistance, but HSS provides higher fracture toughness. If a cutter repeatedly enters and exits a slot, crosses a casting skin, or encounters interrupted stock, HSS may survive impacts that would chip a carbide edge.
Cutting speed, feed, and productivity
Cutting speed is calculated from spindle speed and cutter diameter:
[ V_c = \frac{\pi \times D \times n}{1000} ]
where (V_c) is cutting speed in meters per minute, (D) is cutter diameter in millimeters, and (n) is spindle speed in revolutions per minute. Feed rate can then be estimated using:
[ V_f = f_z \times z \times n ]
where (f_z) is feed per tooth and (z) is the number of flutes.
For the same diameter and workpiece, carbide often permits approximately 2–5 times the cutting speed of HSS when the machine, holder, coolant, and workholding can support it. The actual value depends on alloy, coating, radial engagement, axial depth, cutter diameter, and chip load. Increasing speed without maintaining sufficient feed per tooth can cause rubbing, heat buildup, premature edge wear, and poor finish.
HSS remains practical when the machine cannot reach carbide’s recommended speed. A 3,000-RPM benchtop mill may not fully use a small carbide end mill designed for a much faster spindle, especially when the cutter diameter is large. In that situation, HSS end mills for manual milling machines may provide more predictable cutting at a lower spindle speed.
Tool life and surface finish
Tool life depends on wear mode, not only on elapsed cutting time. Abrasion, built-up edge, thermal cracking, chipping, flank wear, and deflection can all end a tool’s useful life. Carbide generally delivers longer life in stable, continuous cutting, while HSS may deliver a lower purchase cost and easier recovery through regrinding.
Surface finish is also linked to rigidity and geometry. A carbide tool can produce a very consistent finish at higher speed when runout is controlled below practical limits and the toolholder is suitable. However, a flexible machine may cause carbide chatter, leaving marks or causing edge fracture before the tool reaches its expected life.
HSS can provide a good finish during light finishing passes on manual machines because its toughness tolerates minor vibration. It may still produce more burrs or built-up edge when cutting aluminum or ductile stainless steel unless the tool has a sharp geometry, suitable rake, and adequate lubrication.
Material-Specific Recommendations
Aluminum
For aluminum, I normally select a sharp carbide or HSS cutter with polished flutes and two or three flutes when chip evacuation is the priority. Carbide is useful on CNC machines because its higher speed capability supports productive material removal and can reduce built-up edge when the feed and coolant are correct. HSS can work well for prototypes, low-speed machines, and small quantities, especially when the operator can monitor chip formation manually.
Too many flutes can restrict chip space in gummy aluminum. A large axial depth or narrow slot can pack chips into the flutes, causing heat and edge damage. I would prioritize flute polish, helix, chip clearance, and lubrication before choosing between carbide and HSS solely by material grade.
Stainless steel
Stainless steel can be machined with HSS, particularly cobalt HSS, when the cut is light, the spindle speed is controlled, and the tool remains engaged rather than rubbing. The operator must maintain a positive feed because dwelling can work-harden the surface. Carbide is usually preferred for continuous CNC work because it supports higher speed and resists heat-related wear more effectively.
For stainless steel, a strong edge is important, but an excessively blunt edge can increase cutting force and heat. Coated carbide may improve wear resistance, while a sharp, properly relieved cobalt HSS cutter may be safer on an older machine with limited power. The correct choice depends on whether the dominant problem is wear or vibration.
Hardened steel and abrasive materials
Carbide is generally the practical choice for hardened steel, cast iron, powder-metal materials, and abrasive alloys. Its hardness allows the edge to resist wear at cutting conditions that would quickly dull standard HSS. For hardened workpieces, I also consider solid carbide, carbide-tipped, or indexable cutters with geometry designed for the hardness range.
HSS may still be suitable for pre-hardening operations, shallow cuts, drilling-related milling tasks, or repair work where the machine cannot maintain the required speed. It is not automatically unsuitable, but its cutting speed and tool-life limits must be included in the process plan.
Intermediate Choices Between Carbide and HSS
The choice is not limited to solid carbide versus conventional HSS. I often consider four intermediate options when the machine or workpiece does not fit either extreme.
- Carbide-tipped tools: A steel body supports a carbide cutting portion, combining some impact resistance with improved wear resistance. These tools can be practical for larger diameters, interrupted cuts, or heavy roughing.
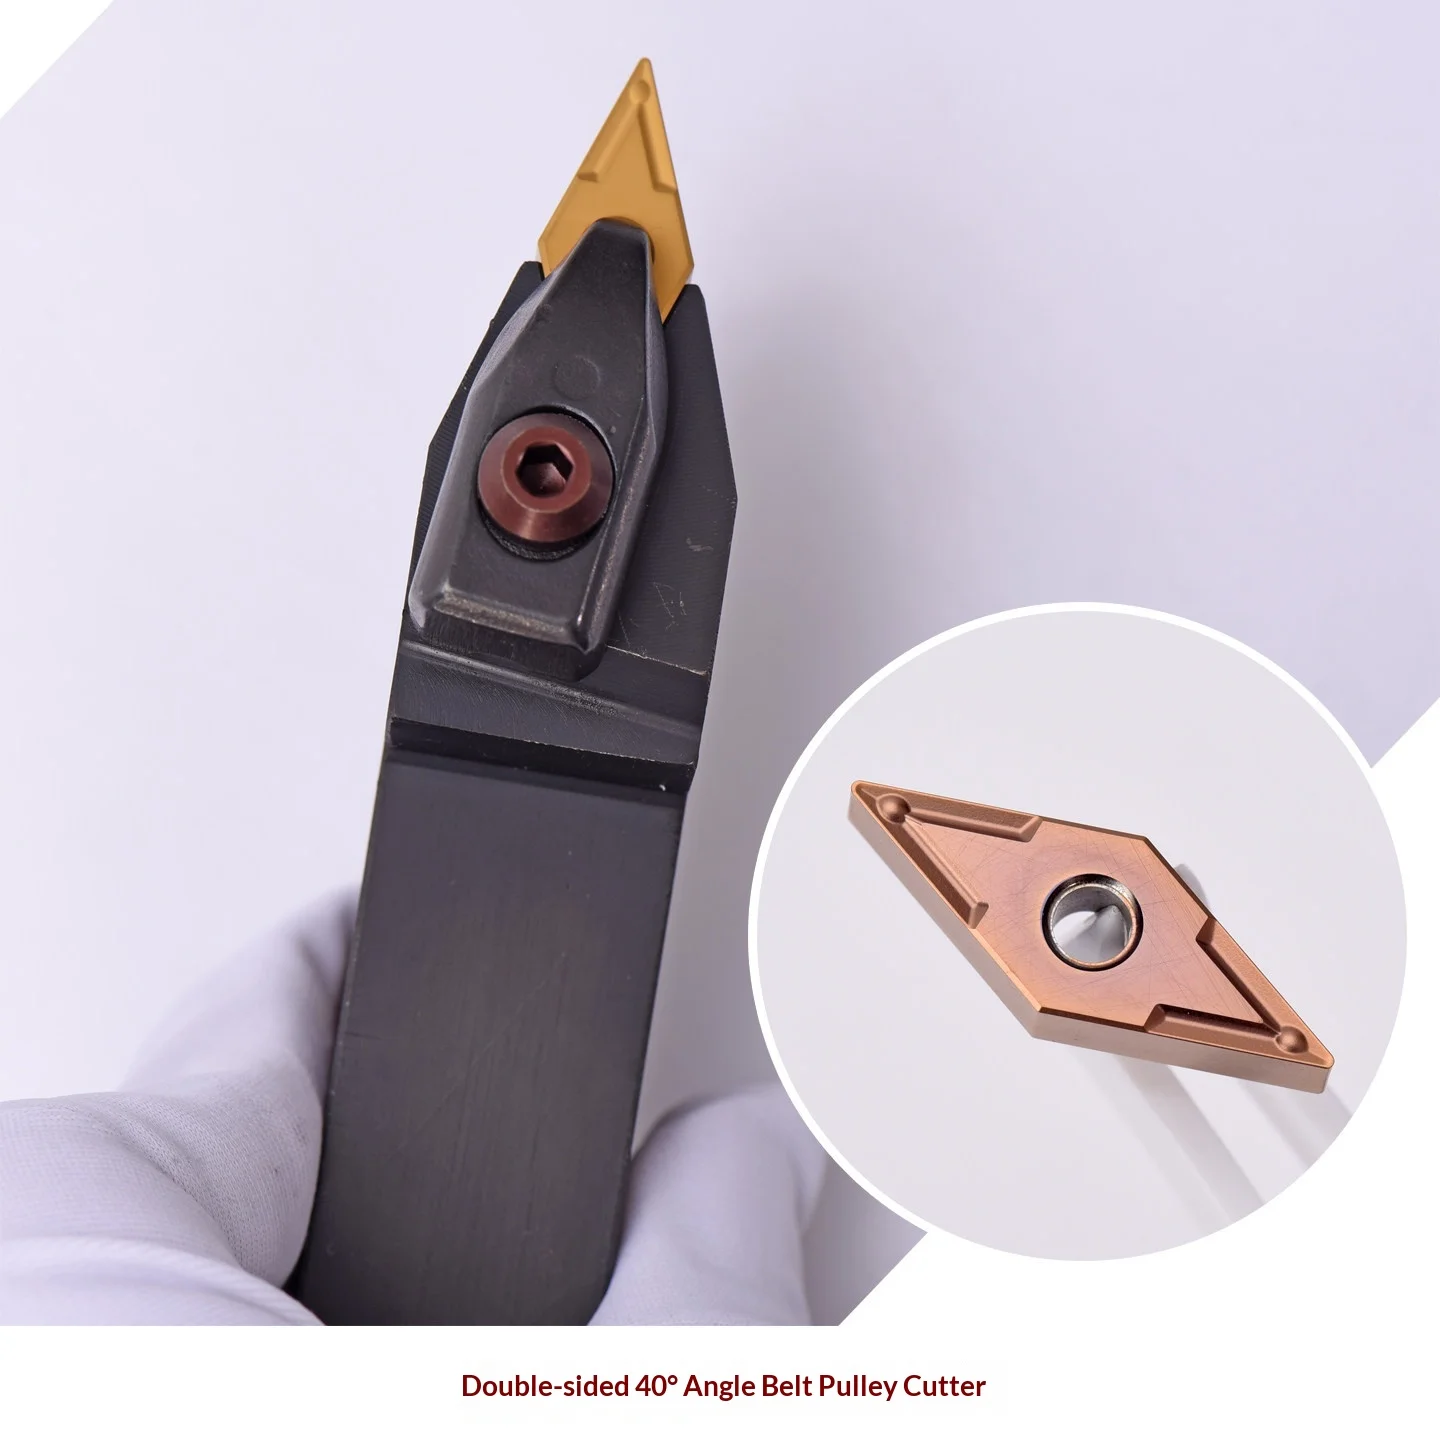
- Indexable milling cutters: Replaceable inserts reduce regrinding requirements and can lower downtime when multiple edges are available. They are suitable for face milling, shoulder milling, and larger material-removal operations.
- Cobalt HSS: Cobalt improves heat resistance compared with standard HSS and is useful for stainless steel, nickel alloys, and moderate-speed work.
- Powder-metal HSS: Powder processing can produce a more uniform structure and better edge strength than conventional HSS, making it useful for demanding manual or moderate-speed applications.
KEUE CNC offers a broader cutting-tool range than a single end-mill material category, including milling cutters, milling inserts, carbide products, turning tools, drilling tools, collets, and tooling systems. When I evaluate a supplier, I look for the ability to match tool material with coating, size, precision, and workpiece drawings rather than treating every application as a standard catalog purchase. KEUE CNC also presents regrinding, technical support, production improvement, and customized tool development as parts of its service structure.
Decision Matrix by Machine and Production Situation
| Operating situation | Preferred starting point | Reason |
|---|---|---|
| Rigid production CNC with high spindle speed | Coated solid carbide | Supports higher speed, chip load, tool life, and repeatability |
| Rigid CNC machining hardened steel | Solid carbide or specialized carbide grade | Resists abrasive and thermal wear |
| Benchtop CNC with limited rigidity | Short, sharp carbide or cobalt HSS | Balances edge performance with vibration risk |
| Manual knee mill | HSS, cobalt HSS, or carbide for stable light cuts | Lower speed and operator-controlled engagement favor toughness |
| Low-RPM equipment | HSS or cobalt HSS | Works effectively at lower surface speeds |
| Interrupted cuts or castings | HSS, carbide-tipped, or reinforced indexable tooling | Better tolerance of impact and variable stock |
| High-volume aluminum production | Sharp coated or polished carbide | Supports high feed rates and chip evacuation |
| One-off repair work | HSS or regrindable tooling | Lower initial cost and easier modification |
| Long overhang | HSS for impact tolerance, or specialized carbide with reduced engagement | Tool choice must address deflection and chatter |
| Strict cycle-time target | Carbide | Higher speed and feed potential can reduce machining time |
Troubleshooting: Match the Failure to the Tool Material
Chatter and vibration
Chatter is usually caused by insufficient rigidity, excessive tool overhang, incorrect speed, poor workholding, or an unsuitable radial engagement. If a carbide tool chips during chatter, switching directly to another carbide grade may not solve the problem. I first reduce overhang, improve clamping, lower radial engagement, and test a speed change; if vibration remains, tougher HSS or carbide-tipped tooling may be more appropriate.
Edge chipping
Chipping commonly indicates impact, excessive feed per tooth, runout, a weak edge preparation, or interrupted engagement. Carbide is especially sensitive to sudden impact because its hardness comes with lower fracture toughness than HSS. I would inspect the holder, reduce feed during entry, use a stronger edge preparation, and consider cobalt HSS or an indexable cutter for unstable cuts.
Rubbing and excess heat
A shiny workpiece, blue chips, squealing, and rapid flank wear often indicate rubbing rather than cutting. Causes include insufficient feed, excessive spindle speed, a dull edge, poor chip evacuation, or a cutter diameter that is too large for the machine. I correct chip load first, then adjust speed and coolant; changing from HSS to carbide without correcting rubbing can shorten carbide life quickly.
Poor surface finish
Poor finish may result from runout, deflection, worn margins, too few or too many flutes, unstable workholding, or incorrect finishing allowance. Carbide can improve finish when the machine is rigid and the cutting parameters are appropriate, but HSS may perform better on a flexible manual machine during a light finishing pass. I separate roughing and finishing tools instead of expecting one geometry to perform both tasks equally.
Premature wear
Premature wear on HSS usually points to excessive cutting speed, insufficient coolant, work-hardening, or an unsuitable alloy. Premature wear on carbide may result from thermal shock, edge chipping, excessive vibration, or coating failure. I record spindle speed, feed rate, axial depth, radial engagement, coolant method, and cutting time so that tool-life comparisons use actual process data rather than purchase price alone.
Practical Cost and Cycle-Time Comparison
A useful comparison uses cost per finished part rather than cost per cutter. I calculate:
[ \text{Tool cost per part} = \frac{\text{Tool price} + \text{regrinding cost} + \text{tool-change labor}}{\text{usable parts per tool}} ]
Then I add machine cost:
[ \text{Total cost per part} = \text{Tool cost per part} + \text{Machine rate} \times \text{Cycle time} ]
For example, suppose an HSS end mill costs $25, produces 20 parts, and requires one 4-minute tool change. A carbide end mill costs $85, produces 100 parts, and requires one 2-minute tool change. If the machine rate is $60 per hour, the HSS tool cost is $1.25 per part before tool-change time, while carbide is $0.85 per part.
The carbide tool becomes more attractive when its cycle-time reduction is significant. If HSS requires 12 minutes per part and carbide requires 7 minutes, the five-minute saving equals $5 per part at a $60-per-hour machine rate. Even with a higher purchase price, carbide can reduce total cost when production volume is sufficient and the machine can hold the required parameters.
For a small machine shop producing only five parts, the calculation may favor HSS because the available carbide capacity cannot be used. For 500 parts, a rigid CNC, and repeatable workholding, carbide usually receives a stronger economic case because tool life, fewer changes, and shorter cycle time compound across the batch.
Which Alternative Should You Choose?
| Your priority | Recommended choice | Why |
|---|---|---|
| Lowest initial cutter price | Standard HSS | Suitable for low-volume and low-speed work |
| Manual milling and interrupted cuts | Cobalt HSS | Tougher edge with better heat resistance than standard HSS |
| High-speed CNC production | Coated solid carbide | Higher speed, feed, and wear resistance |
| Large-diameter roughing | Indexable or carbide-tipped cutter | Multiple edges and stronger bodies support material removal |
| Flexible benchtop CNC | Short carbide or cobalt HSS | Balances cutting ability with vibration tolerance |
| Hardened steel | Solid carbide | Better resistance to abrasion and heat |
| Frequent tool reconditioning | HSS | Easier and generally less costly to regrind |
| Long production runs | Carbide or indexable tooling | Lower tool-change frequency and greater process consistency |
| Unstable castings or welded assemblies | HSS, carbide-tipped, or reinforced indexable tool | Better tolerance of interrupted engagement |
| Custom dimensions or coatings | Supplier with design support | Tool geometry can be matched to the actual process |
Final Recommendation
Carbide Milling Tools vs HSS Milling Tools: Which Is Better? The answer depends on the machine, material, cutting conditions, and production target. Carbide is the stronger choice for rigid CNC production, hardened steel, abrasive materials, high spindle speeds, shorter cycle times, and longer continuous tool life. HSS is the better fit for manual milling machines, low-RPM equipment, interrupted cuts, flexible setups, prototypes, and budget-controlled low-volume work.
Before purchasing, I would record spindle speed, cutter diameter, material hardness, machine rigidity, tool overhang, expected quantity, and current cycle time. I would then select geometry and coating together with the material, rather than comparing carbide and HSS as isolated categories. For production work, calculate total cost per finished part; for manual or unstable work, prioritize toughness and controllability over theoretical cutting speed. This process gives machinists a defensible choice between Carbide Milling Tools, HSS, cobalt HSS, carbide-tipped, and indexable solutions.